Manufacturing Production Solutions

The training strategies that keep energy project teams deployment-ready

Industrial contractors working across oil, gas and renewable energy often rely on the same engineering workforce to deliver projects with different operational requirements. A maintenance team may complete work at an onshore processing facility before moving to an offshore installation, while another group prepares for a wind-energy contract. These transitions require careful resource planning because employees need the appropriate safety training for each assignment. When training is scheduled too late, contractors can have qualified engineers available but still be unable to mobilise them.

Match training requirements to the project pipeline

Workforce planning should begin with confirmed and anticipated contracts. Each project allows managers to identify the personnel required, their working environment and the safety training needed before deployment. Establishing these requirements early helps employers schedule training alongside other project activities.

For offshore oil and gas assignments, the Offshore Petroleum Industry Training Organisation (OPITO) develops internationally recognised training standards covering offshore safety, emergency response and technical activities. Completing the relevant OPITO training courses  prepares personnel for the safety requirements of their assignments, including initial offshore safety training for employees who have not previously worked offshore.

The OPITO framework  gives employers a consistent basis for establishing training requirements across different offshore roles. Contractors can then identify which employees need additional preparation and schedule training around existing operational commitments.

Prepare personnel for upcoming wind-energy contracts

An industrial contractor expanding into wind energy may already employ engineers with relevant mechanical or electrical expertise. Their experience provides a foundation for turbine installation and maintenance, but working on wind turbines introduces additional safety requirements, particularly around elevated access and emergency response.

The Global Wind Organisation (GWO) develops internationally recognised training standards for the wind energy sector. Its safety training covers working at height, first aid, fire awareness and manual handling, with additional sea-survival training for offshore personnel. Completing the relevant GWO courses  allows experienced industrial engineers to develop the safety skills needed for wind turbine work while building on their existing technical knowledge.

For operations managers, the transition into wind energy creates an opportunity to make better use of the workforce between contracts. Engineers approaching the end of an industrial maintenance assignment could complete wind-specific training before moving to their next project.

The Global Wind Organisation's training standards  help employers identify the training relevant to upcoming assignments, allowing them to prepare personnel for new projects without unnecessarily disrupting existing operations.

Include training in workforce capacity planning

Training affects the number of productive engineering days available to a business. When several employees attend courses simultaneously, the remaining workforce must still meet existing project commitments.

A resource plan should therefore account for training alongside project delivery. It should identify:

  • Personnel required for each project and their deployment dates.
  • Training that must be completed before mobilisation.
  • Existing commitments that determine when employees can attend training.
  • Availability of qualified personnel to cover operational duties during training periods.

This provides managers with a clearer picture of workforce capacity and allows training costs and employee availability to be incorporated into project estimates.

Keep training records aligned with deployment schedules

Certain safety qualifications require periodic renewal, meaning employees who were available for an earlier project may need refresher training before their next assignment.

Recording qualification expiry dates against future project allocations helps managers identify these requirements early. Training can then be arranged during quieter operational periods or between assignments.

A central workforce schedule containing training records, expiry dates and confirmed course bookings makes this information accessible to operations and project management teams.

For wind-energy projects, the Global Wind Organisation's WINDA database  provides a central system for recording and verifying completed GWO training. Employers can use these records to confirm training status before allocating personnel to upcoming contracts.

Coordinate subcontractor readiness with project delivery

Industrial projects frequently depend on specialist subcontractors whose personnel must meet applicable training and mobilisation requirements.

These requirements should be established when subcontractors are appointed. Project teams need to understand which competencies the subcontractor will provide and whether additional training is required for the destination asset.

An experienced subcontractor may have the technical expertise to perform the work but need further preparation for a different offshore or wind-energy environment. Confirming these requirements during procurement reduces the risk of discovering outstanding training needs immediately before deployment.

Make workforce readiness part of project delivery

Effective training planning gives contractors a clear picture of employee availability and readiness across upcoming contracts. By incorporating training requirements into project schedules, businesses can maintain operational capacity while preparing their workforce for assignments across oil, gas and wind energy.

All GWO Training Courses | Train when it suits you at FMTC Safety
Pipe dreams become a lifting reality with turnkey Hoist & Winch package

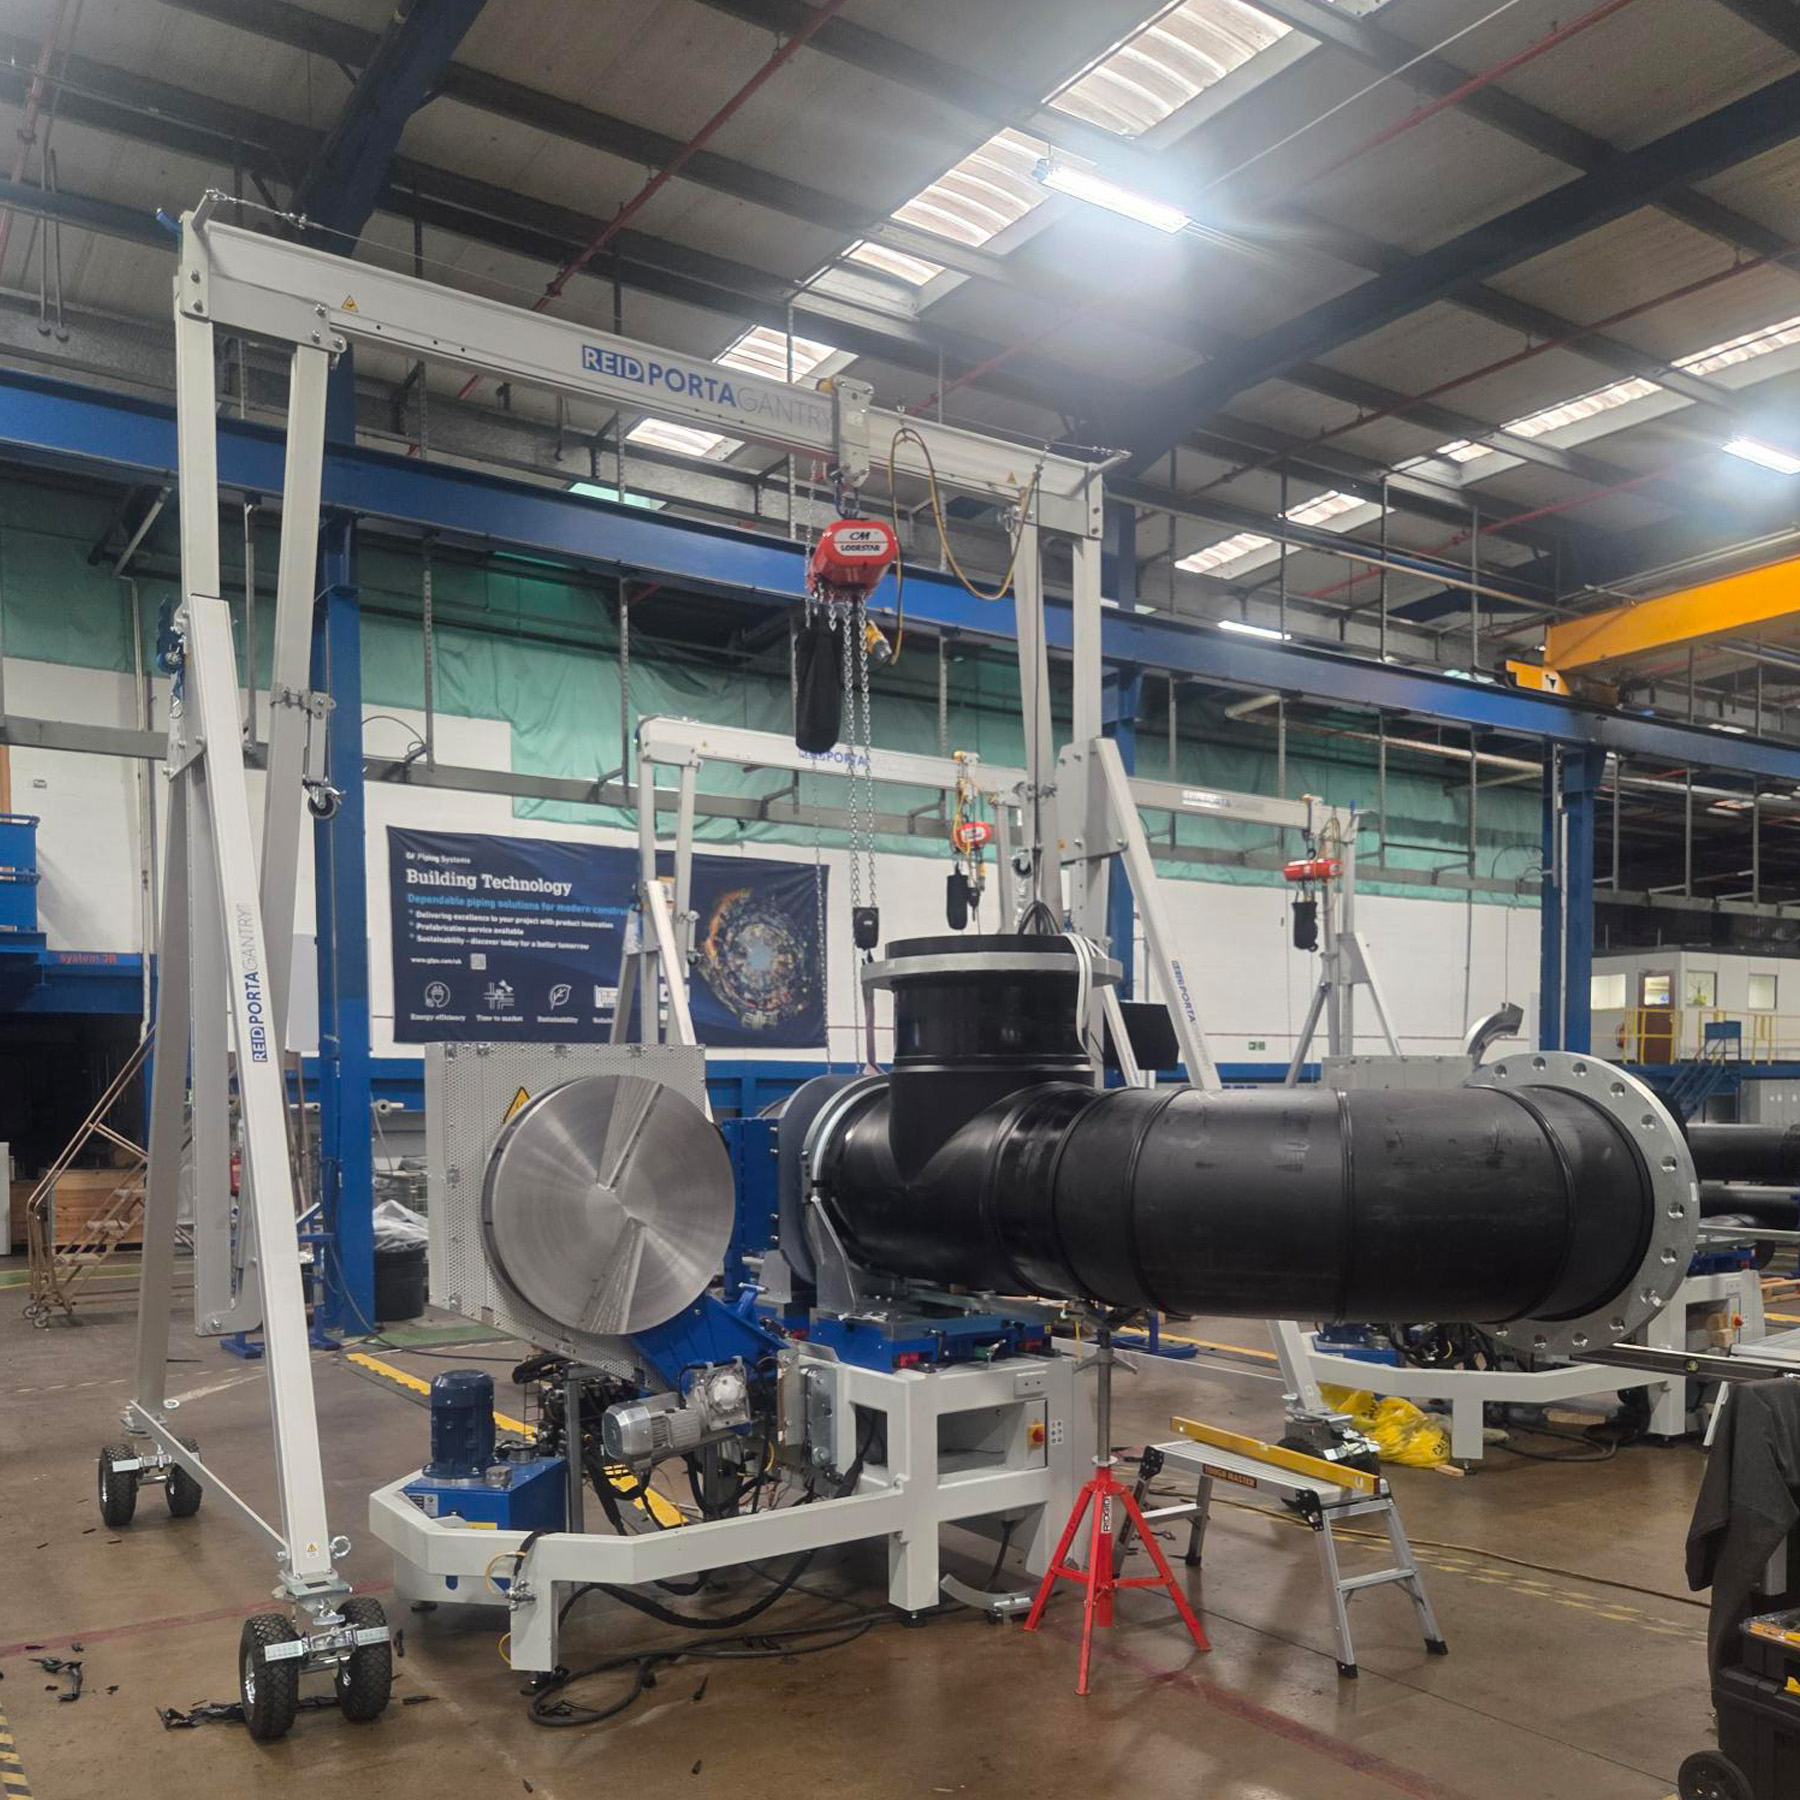
For a UK-based manufacturer of plastic pipe systems, flexibility is essential when handling large-section pipework and the customised angle and bend connections required by end customers. To support final assembly operations, Hoist & Winch Ltd has supplied and commissioned a turnkey package of eight aluminium mobile gantry cranes offering 2-ton safe working load (Swl), each equipped with a 110V single-phase electric chain hoist.

The equipment is installed in a dedicated section of the manufacturer's final assembly area, where pipe sections – used to protect electrical cables – are fitted with angle and bend connections.

The company supplies customers across a wide range of industries, including the growing datacentre sector. Flexibility was therefore a key consideration in the specification. Manufactured by Reid Lifting, the aluminium mobile gantries supplied by Hoist & Winch feature adjustable height and span width, allowing the configuration of each crane to suit the available workspace and the dimensions of the pipes that require handling.

With a maximum working hook height of 6 metres and bridge span of 4 metres, the cranes provide sufficient capacity and reach for the largest pipe sections currently processed by the company. They also offer an element of future-proofing should the manufacturer introduce larger sections.

Mobility is another critical feature. Each gantry features large pneumatic-tyred wheels, making the cranes easier to manoeuvre while improving stability when travelling under load. This capability is particularly useful when moving across raised cable ramps or small floor imperfections.

The four wheels incorporate 360-degree swivel action with directional locking at 90-degree intervals, providing operators with further flexibility when positioning the gantries. Once correctly positioned over the workstation assembly jigs, manually operated heavy-duty parking brakes securely hold each crane in place. Here, the lifting systems play a vital role in the assembly process, safely supporting pipe sections while angle or bend connections are fitted and adhesives are allowed to cure.

“It's a deceptively demanding application because the lifting equipment needs to combine substantial capacity with the freedom to move around the assembly area,” explains Hoist & Winch Director Andy Allen. “The aluminium gantries give the customer that flexibility, while the 2-ton Swl hoists offer the reliable lifting performance needed for these large and varied pipe sections.”

To provide effective and electrically safe lifting within the assembly environment, Hoist & Winch installed heavy-duty 2-ton Swl Yale/Loadstar 110V single-phase electric chain hoists. The low-voltage supply is particularly appropriate because the gantries require powering via a trailing floor cable as the company moves them between workstations. Hoist and pendant control cables are managed across each crane bridge using a taut-wire festoon catenary system, helping to maintain orderly cable routing while allowing the hoists to travel along the bridge.

Following installation, Hoist & Winch completed LOLER (Lifting Operations and Lifting Equipment Regulations) inspection and testing of each complete lifting system and issued the appropriate LOLER Thorough Examination reports, providing complete peace of mind for the customer.

On-site operator training covered equipment functionality, hoist components and operating controls, including top and bottom limit switches and emergency-stop functions. Training also addressed periodic checks and lubrication, together with annual inspection, servicing and certification requirements. Each operator was given practical experience in using the equipment, ensuring safe and effective operation of the new lifting systems from day one.

Visit //lnk.ie/7FDA8/e=This email address is being protected from spambots. You need JavaScript enabled to view it./https:/www.hoistandwinch.co.uk" title="https://lnk.ie/7FDA8/e=This email address is being protected from spambots. You need JavaScript enabled to view it./https:/www.hoistandwinch.co.uk" data-auth="NotApplicable" data-linkindex="5">www.hoistandwinch.co.uk for further information and to view recent case studies.

Faster asset audits & interventions

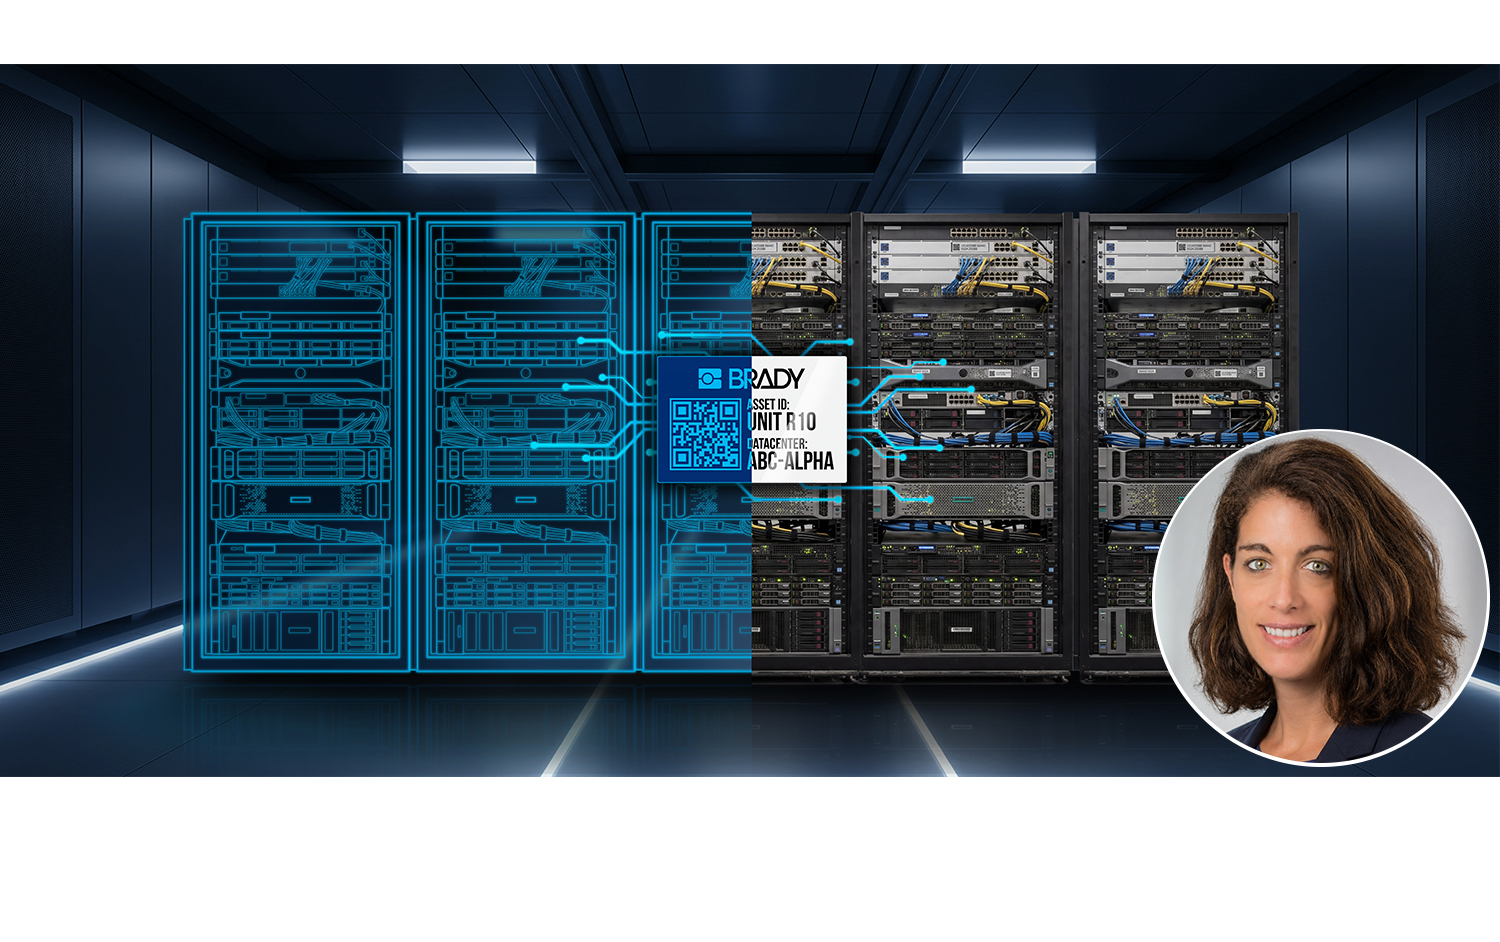
Many data centres are increasing asset density to support growing demand for computational power, driven by AI and Internet of Things-applications. How are data centres managing all these physical assets?

DatacentreTwinLinda

Higher data centre asset densities

More apps, more connectivity. Billions of people talking to each other via technology, joined by trillions of things. All that interaction needs computation. Add to that artificial intelligence algorithms that need gigantic, and growing, computational power. These trends have clear consequences for data centre infrastructure. They require more cables. More servers. More ports. Higher density racks. And larger server rooms in bigger data centres.

“How to maintain efficiency for moves, adds and changes on so many assets? That is a question we regularly hear when talking to data centre managers”, said Linda Chochoy, Product Manager Market Development at Brady Corporation, a supplier of automated identification and data capture solutions. “How to keep physical asset audits feasible? How to keep the data centre’s real world, tangible assets aligned with its DCIM or core asset databases?”

“A great, tried and tested way to manage overwhelming and growing numbers of assets is automation with machine readable serial numbers or barcodes. When scanned, they instantly generate digital data and can connect a specific physical asset to the right digital record. The barcode’s advanced siblings, the datamatrix and QR-code, are even better suited for very high density asset environments. They allow data parsing, and enable multiple, automated and fast applications based on the same code. If that is not yet fast enough however, if you need asset identification hyperspeed, label-integrated UHF RFID technology is the nec plus ultra.” 

Tiny QR or datamatrix codes

“The advantage of barcodes is that, when scanned, they instantly generate a digital data trail. But let’s face the truth: barcodes have been around since the 1960’s. In data centres, they take too much space, require labels that are too large, and as a result they can hardly be used to identify each server port separately. Due to their size, they also need considerable cable flag labels to maintain code legibility. All those large flags can create a big mess, certainly in high density racking.”

“Enter the QR-code or industrial data matrix code. Smaller, able to include more information, these codes can be printed in millimeters while maintaining scanner readability. They can fit tiny cable flags and every port in high density servers, routers and switches.”

“To read these codes, classic retail scanners do not suffice. They require high accuracy image capture devices that can include near-field and far-field technology, or a combination of both. Advanced Linux-based scanners exist that feature native JavaScript to enable hundreds of custom, user-defined applications. To create labels for these applications, using tiny, high-resolution datamatrix and QR-codes, high accuracy and high precision label printers are needed that can print 203 or even 600 dots per inch (DPI). Printers can be set up to print asset codes straight from your systems as a QR- or datamatrix code on reliable, machine readable labels.”

The importance of tag and label reliability

Some data centre managers have become wary of using labels because of negative experiences. Labels take time to create and apply, and when they are about to pay off, lower quality labels can be found at the bottom of the server rack.

Screenshot 2026 09 03 104139

“Labels that cannot stay attached serve no purpose at all. A data centre is a challenging environment that requires professional, quality labels. Server-generated heat is detrimental to lesser label adhesives. In addition, curved cable surfaces require specialised label materials. Brady has researched and developed a range of professional labels made out of nylon cloth and advanced polymers. These labels can keep all data centre cables and components identified. Laboratory-testing, using internationally accepted FINAT- and ASTM-methods indicate they stay attached and remain legible for up to 10 years in data centre environments. That’s more than the lifecycle of most data centre assets.”

5 outcomes for well identified data centres

A well-identified data centre has every cable identified, including all fibre, UTP, power and other utility cables. All server, router and switch ports will also have a unique, coded identity. This enables DCIM or system updates with just two 1 second code scans: scan cable, scan port.

“Well-identified data centres enable 5 considerable benefits:

  • More accurate and faster moves, adds and changes (MACs), through faster identification of the right assets, with greatly reduced risk of unplugging the wrong cable
  • Faster troubleshooting with clear identification on every cable and asset
  • Faster rack and server room audits by scanning physical assets against digital infrastructure records or DCIM-data
  • Faster, feasible data centre inventory checks
  • More smoothless server rack commissioning and decommissioning

Next to cable and port identification, many higher tier data centres also label transformers, pipes and other infrastructure to increase the speed and precision of a wider range of interventions that may be required to protect uptime and high service levels.”

RFID: a physical asset radar

To achieve even higher asset identification speed, RFID technology is the top of the line. Instead of scanning each asset’s code, RFID readers will detect all assets in range in a single scan. Passive, UHF RFID labels do not require batteries and feature thin, integrated antennas that provide up to 15 metres read range in open spaces.

“Brady offers specialised on-metal RFID labels that circumvent known radiosignal distortion from metal surfaces. Read range in datacentres is about 3-4 metres, more than enough to very quickly confirm the presence of labelled assets in multiple server racks in a couple of seconds.”

“The technology works like radar, in a sense that the labels bounce off radiosignals emitted from UHF RFID readers. A portable RFID reader enables users to select a detected asset’s ID number on-screen and to write to that tag or to its record. 

Through signal strength variation detection, it is even possible to home in on a selected asset with on-board visuals and sounds.”

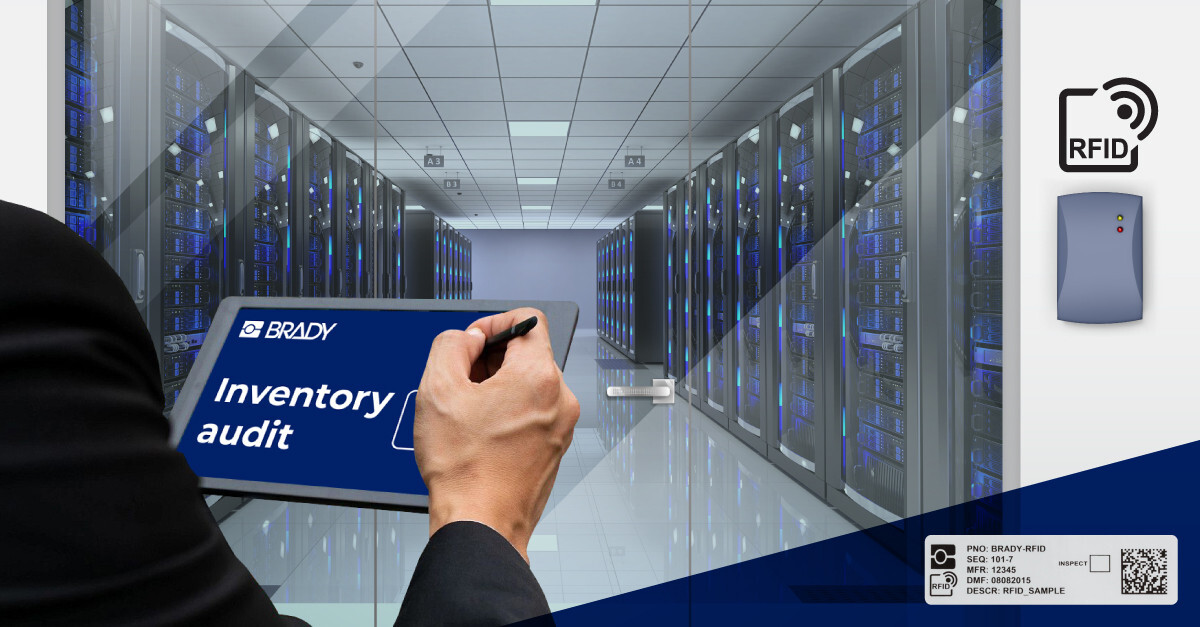
“There is more. If fixed RFID readers are placed at server room entrances, every labelled asset moving in or out can be detected automatically, along with its movement direction. This makes it possible for data centres to automatically update server room inventory lists, to sound a buzzer or send a text message when the wrong asset moves in or out, and to enable server room inventory checks and audits in a minimum of time.”

RFID data centre inventory audit Europe English

Webinar: Datacenter lifecycle identification

How to optimally support efficiency goals across the data centre life cycle? Discover the role of reliable identification in data centre construction, commissioning, hand-over and lifecycle operations.

Topics:

  • Design & build: support compliance, high durability and smart traceability
  • Commissioning: enable high speed execution
  • Handover: quickly reconcile physical asset labels with digital records
  • Lifecycle operations: protect uptime and facility ROI
  • Fill out the form and get your free recording of the data centre identification and traceability webinar.

Get the webinar recording now >>

Brady Corporation

This email address is being protected from spambots. You need JavaScript enabled to view it.

www.brady.co.uk

Picture2

Linda Chochoy works as Product Manager Market Development for Brady Europe, Middle East and Africa. She analyses customer needs, interviews data centre managers, cable harness production managers and electronics production managers to capture emerging business needs and support Brady’s product development.


Pepperl+Fuchs introduces new industrial-grade ruggedized tablet series

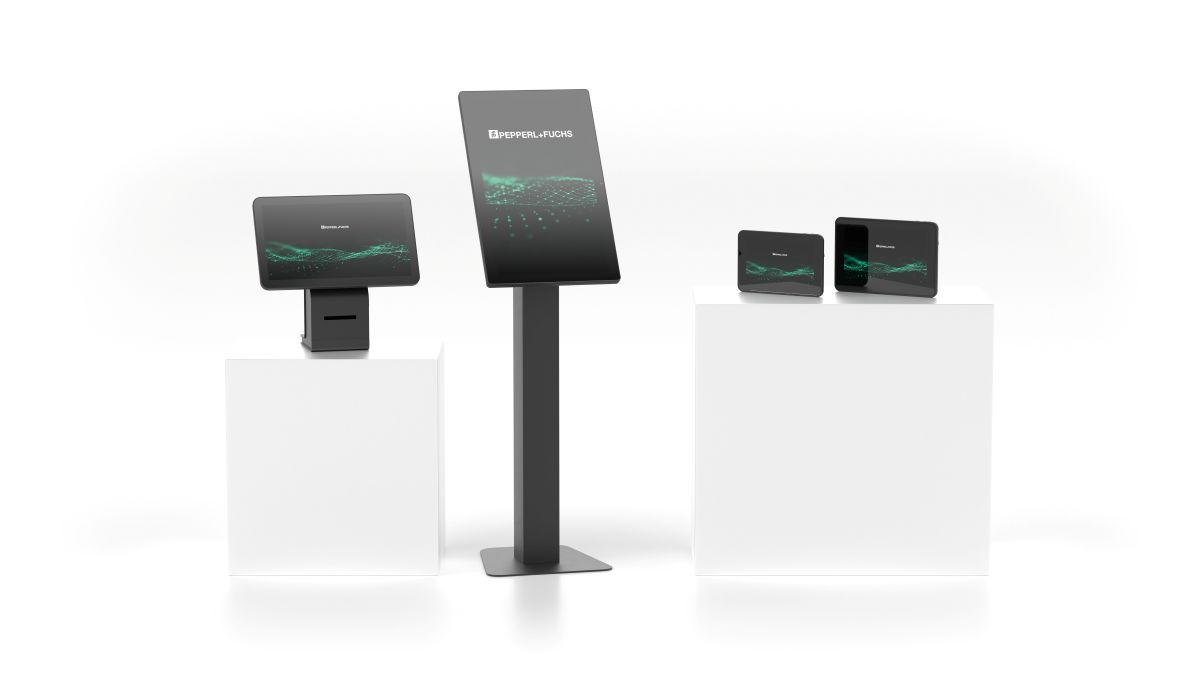
The Tab-IND series complements the Pepperl+Fuchs enterprise mobility portfolio with rugged industrial tablet solutions for intralogistics, the manufacturing and automotive industries, and field applications.

Pepperl+Fuchs, specialist for enterprise mobility solutions for industrial hazardous and non-hazardous areas, is introducing its new Tab-IND series of tablets with 8 and 10-inch displays for industrial use, leveraging its expertise in hazardous areas requirements. The rugged devices are protected against dust and spray water according to IP65.

The Tab-IND series is designed for applications in industrial environments where mobile devices are subjected to harsh conditions and where a long service life and flexible customization options are required – such as in intralogistics, manufacturing, or the automotive industry. The Tab-IND’s extensive range of accessories and available interfaces allow the tablet to be customized for specific application needs.

The tablets ship with Windows 11 or Android 15 (10-inch model only), but are also available with a ThinClient. Bright displays with up to 700 cd/m², stylus and glove support, and an operating temperature range of -20 °C to +50 °C enable use in harsh industrial and outdoor environments. All variants feature a 13-megapixel main camera. The Windows models are additionally equipped with a 13-megapixel front camera, while the Android version features a 5-megapixel front camera.

Connectivity is ensured by the latest mobile and communication standards such as Wi-Fi 6E, Bluetooth 5.3 BLE, 5G, or LTE. A front-facing NFC module supports, among other things, access and identity controls for restricted areas. In addition, Push-to-Talk over Cellular enables fast and easy voice communication for groups over cellular networks, while a freely programmable button and a fingerprint sensor ensure flexible use and secure authentication.

With a quad-core processor, up to 16 GB of RAM, and up to 256 GB of internal storage, the tablets are ideally equipped for modern augmented reality and extended reality applications. The removable battery with a capacity of 37.2 Wh provides up to 14 hours of runtime. Weighing just over 500 grams (8-inch) or just over 800 grams (10-inch), the tablets are also slim and lightweight.

SmartBacks expand the range of functions

To expand the Tab-IND series, Pepperl+Fuchs offers various SmartBacks. These are attached to the back of the tablets and expand the range of functions depending on the application. Additional batteries to extend runtime or special mounts can also be added as SmartBacks to the back of the device. Custom extensions based on SmartBack technology are also possible, such as for communication interfaces like Industrial Ethernet or IO-Link.

Among other things, a scanner frame is available for barcode scanning, for tracking shipments, or for picking materials or goods to support efficient intra- and transport logistics processes.

Additional accessory solutions are available, such as vehicle mounts, anti-theft devices, rugged frames for increased durability, charging stations with multiple charging bays, or a mount/single bay. The devices are charged via durable contacts on the underside, which are particularly long-lasting. An IO dock for use with external devices and displays is also available, making the tablet an alternative to a stationary office PC.

Kiosk terminals for industrial environments

As additional variants, Pepperl+Fuchs offers two kiosk terminals in 15-inch and 22-inch display sizes. They are suitable, for example, for access control, as information displays, or for digital workflow interactions. Both sizes are equipped with Android 15, 8 GB of RAM, 128 GB of internal storage, and a front-facing NFC module. The 22-inch terminal features a 13-megapixel front camera, while an optional 5-megapixel front camera is available for the 15-inch terminal.

European development and local expertise

The new devices complement the existing ultra-ruggedized portfolio of tablets from the Tab-Ex® series and smartphones from the Smart-Ex® series for hazardous areas. Development and design incorporated Pepperl+Fuchs’ expertise as a global market leader and trusted advisor for the most demanding solutions and applications in hazardous areas, leveraging global supply chains.

Pepperl+Fuchs places special emphasis on European development and design to address the specific challenges faced by industrial companies. This means that companies can not only choose between different display sizes but also expect long-term device availability (at least five years) and software updates.

True to the motto “Global but Local,” Pepperl+Fuchs, as a family-owned German company, offers its customers comprehensive service through its local branches in the respective local language. Especially for companies that use tablets in both hazardous areas and simply harsh environments, it is advantageous to be able to source all devices from a single provider.

A strong partner for every task

With Pepperl+Fuchs, customers benefit from a comprehensive portfolio and years of experience, not just in hazardous areas. Mobile devices, HMI solutions, and a wide range of process-oriented devices and sensors come together perfectly to form a broad offering for any automation and digitalization requirements. Mobile workers can integrate additional solution packages from a single source, such as Pepperl+Fuchs data collection, measurement, and monitoring devices, headsets, or Auto-ID.

https://www.pepperl-fuchs.com/

Subcategories

Share This

1 2 3 4 5 6 7 8 9 10 11 11